Quality Control for Molds and Plastic Parts
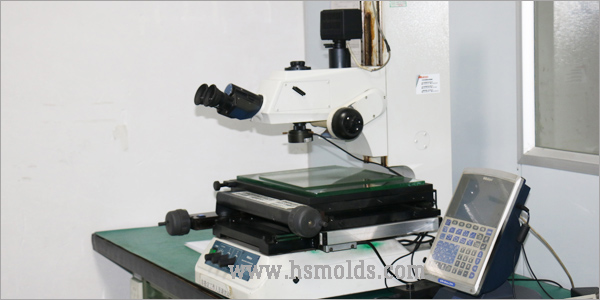
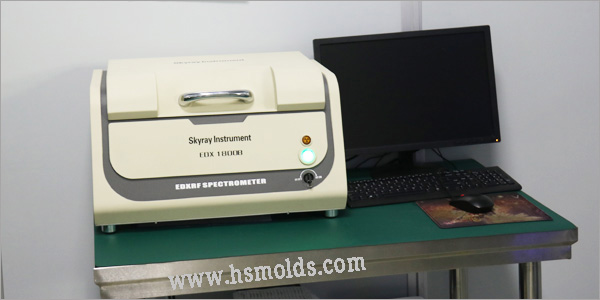
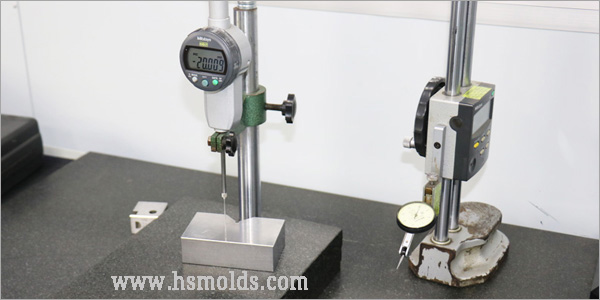
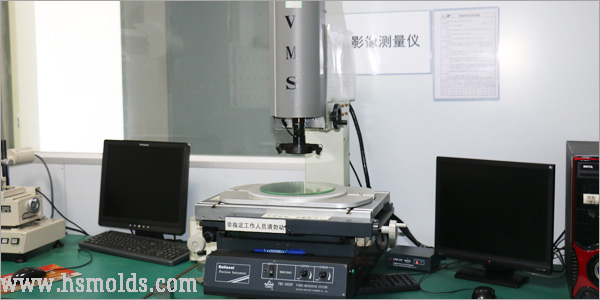
Most of our mold machines are imported to ensure accuracy and quality
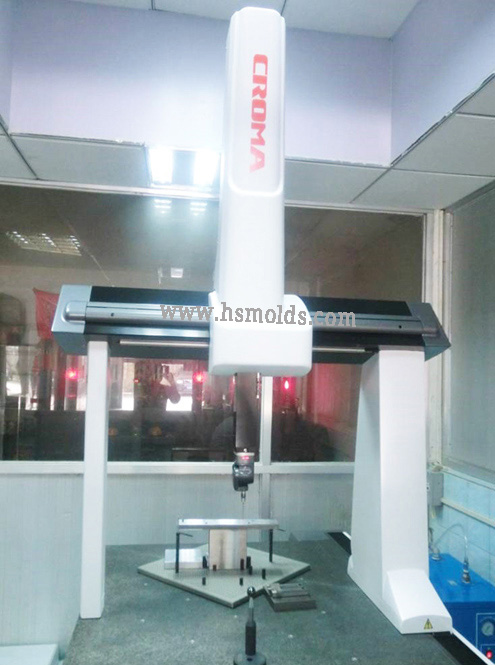
We strive to provide our customers with the highest quality in injection molded plastic products & services. We have implemented ISO quality assurance system to plan, control, measure, and continuously improve our business & molds.
At HS Molds, strict quality standards and inspection procedures are implemented to make sure every part or every component that we manufacture meet your requirement.
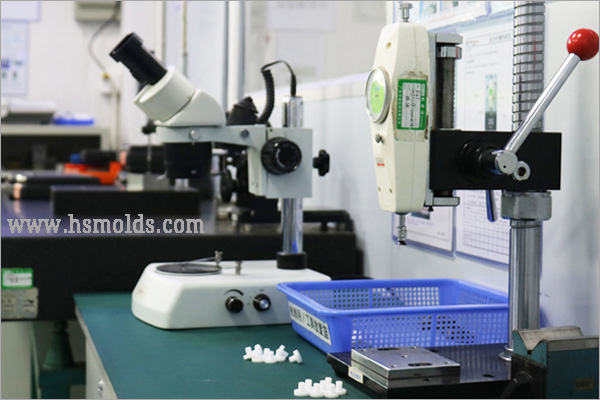
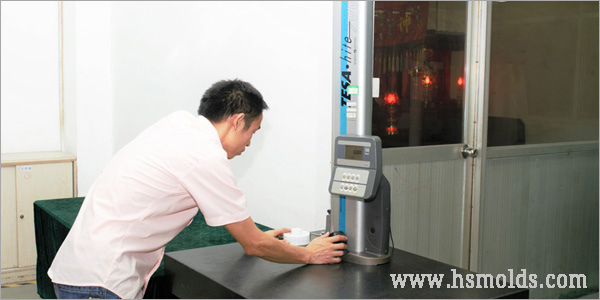
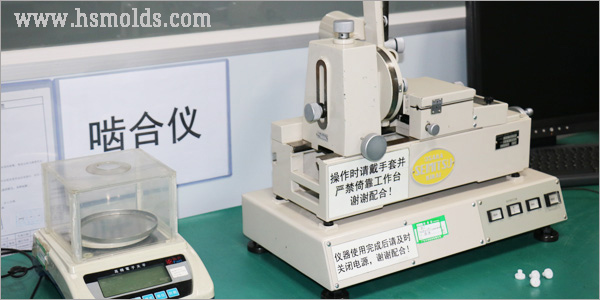
What is in-process inspection in manufacturing?
In-process inspection means checking a part, tool, or operation while manufacturing is still underway. Its purpose is to find variation close to the point where it begins, while the team can still correct the process and prevent the same issue from moving into later operations.
At HS Molds, quality control follows the manufacturing route. A mold insert, molded plastic part, machined component, and assembled product do not need the same checks. The drawing, functional risks, cosmetic standard, material, process, and customer documentation define what is measured and when.
Inspection stages for molds and plastic parts
Incoming and setup verification
Material identity, approved drawings, measurement methods, machine setup, and critical process inputs are confirmed before work begins. This creates a known reference for later inspection.
First article inspection
The first completed piece or trial sample is compared with the defined dimensions, appearance, and functional requirements before the operation moves into repeat production.
In-process inspection
Selected dimensions and visual conditions are checked at planned intervals. Results can expose tool wear, setup movement, molding drift, or handling damage before a full batch is affected.
Final and pre-shipment inspection
Completed parts are checked against the release criteria, including quantity, identification, packaging, required records, and any final dimensional, visual, or functional checks.
Visual, dimensional, and functional inspection
Visual inspection looks for surface and assembly conditions such as flash, sink, flow lines, discoloration, scratches, contamination, incomplete filling, and cosmetic mismatch. Dimensional inspection compares measurable features with the drawing using equipment appropriate to the feature and tolerance. Functional inspection checks how the part fits, moves, seals, assembles, or performs in its intended interface.
No single inspection method proves the quality of every feature. A measurement plan should identify the critical characteristics, the tool or fixture used, the sampling frequency, and the response when a result is outside the defined limit.
How process inspection supports corrective action
When a result is outside the agreed requirement, the affected material is identified and held while the team checks the cause. That review may include machine settings, material condition, fixture or tool wear, measurement method, operator handling, and the history of the last accepted check. Corrective action is then verified with new evidence before production continues.
This closed-loop approach makes quality control useful to manufacturing. Inspection records do more than accept or reject a finished batch; they help engineering, mold making, injection molding, CNC machining, and assembly teams control repeat production.
Review mold fabrication controls See CNC equipment and machining View the connected manufacturing route
Frequently asked questions
What is the difference between in-process and final inspection?
In-process inspection checks selected characteristics while manufacturing is underway so variation can be corrected early. Final inspection confirms that completed parts, records, identification, and packaging meet the defined release requirements.
What does a first article inspection check?
A first article inspection compares the first completed piece or trial sample with the approved drawing and the defined dimensional, visual, and functional requirements before repeat production proceeds.
How are inspection methods selected?
Inspection methods are selected from the feature, tolerance, function, process risk, and customer documentation. The plan should define what is checked, the measuring equipment or fixture, the sampling frequency, and the response to a nonconforming result.